Ingredients Quality
Ingredients Quality
We monitor taste, quality and safety along the making of our products through controls on our ingredients, semi-finished products and finished products globally.
Our quality tasting panel involves over 2500 expert tasters around the world, to verify and guarantee the taste excellence and consistency of our products.
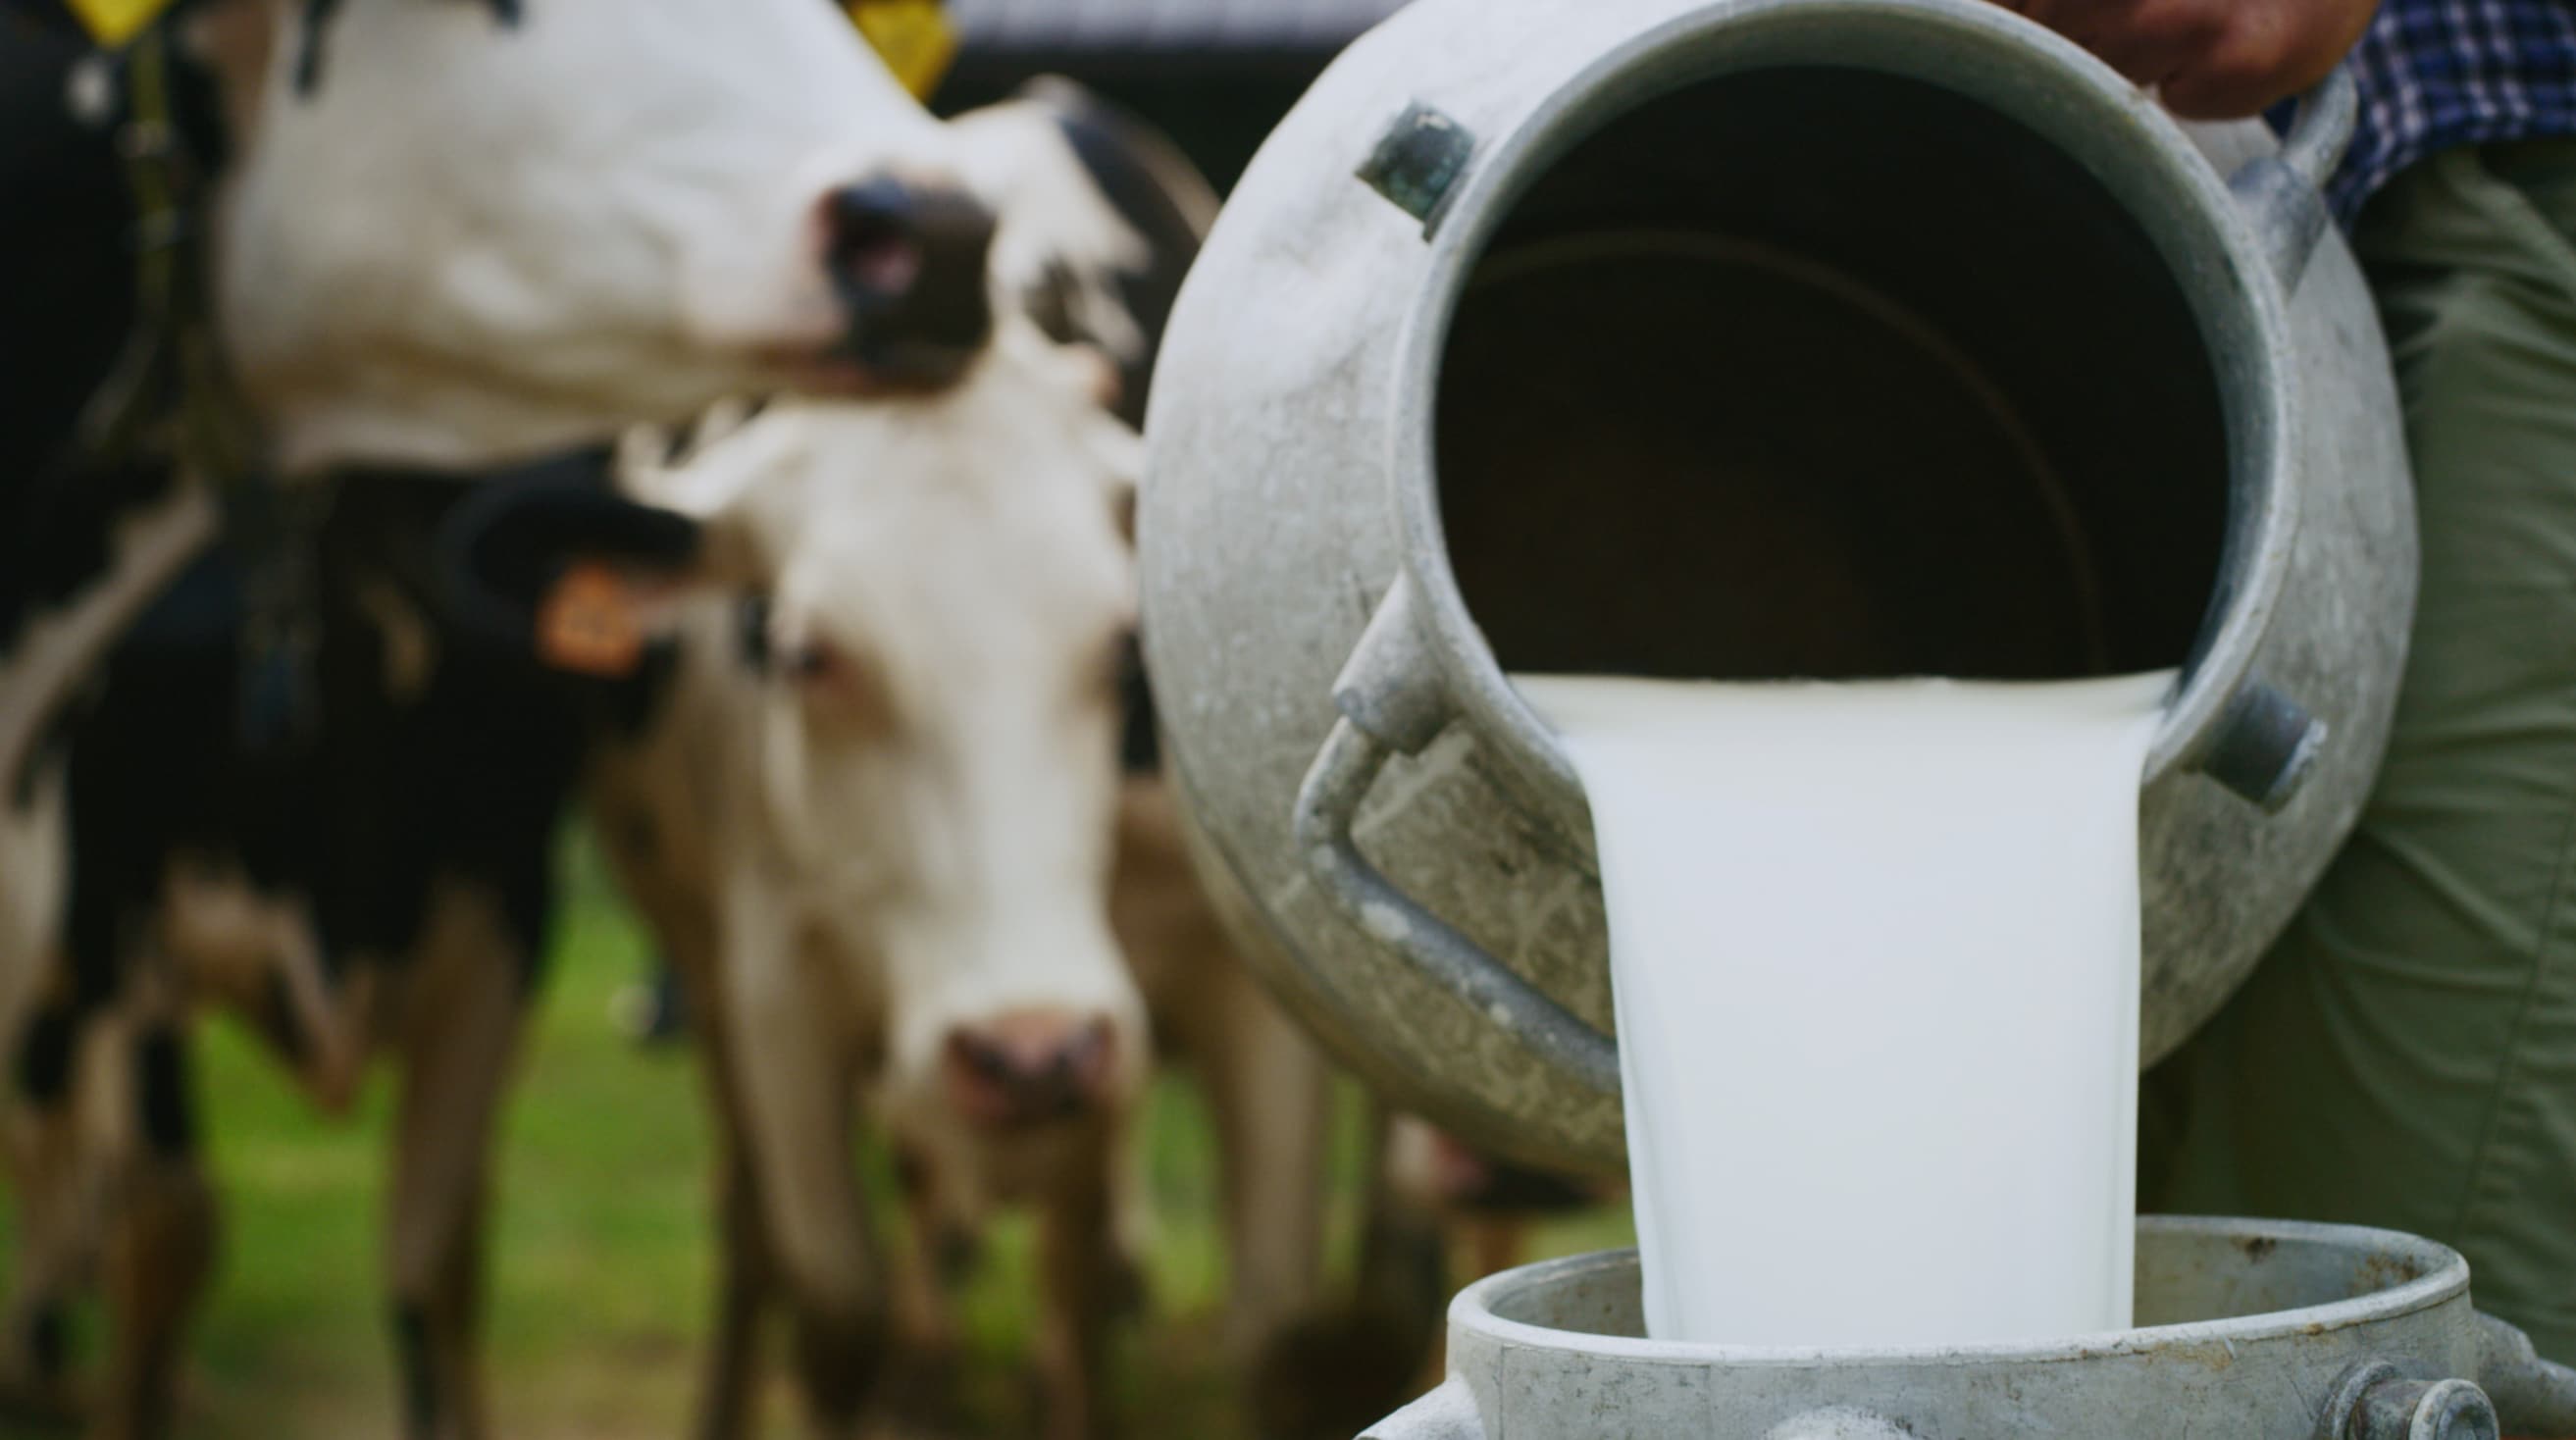
Milk is an important ingredient in many Kinder products, and we take care in selecting it and handling it with attention to quality.
The journey starts at the farm where cows are milked.

The fresh milk is immediately refrigerated in tanks to slow down bacterial growth and maintain its freshness.

The cooled milk is stored in large, insulated bulk tanks at the farm until it is collected.

Specialized insulated tanker trucks collect the milk from farms, keeping it cool during transportation.
Milk is typically collected within 24 to 72 hours from milking to ensure its freshness.

Upon arrival at the dairy, the milk undergoes rigorous quality testing for factors like-visual check, temperature, acidity, and contaminants.

The milk that passes the quality testing is pasteurized bringing it to a defined temperature for a few seconds to kill any harmful bacteria and extend its shelf life.
For some of our products like Kinder Chocolate or Kinder Surprise, we need dried milk. In this case the liquid pasteurized milk is dried through a technique called spray drying, that removes nearly all its water content turning it into a powder.

Both the liquid pasteurized milk and the powdered milk are then transported to our factories, ensuring that they always remain in optimal conditions, and then are mixed with the other ingredients in the different Kinder recipes to create the Kinder products that you love.
- Europe
- NAM
- International
- APAC – MEA
Kinder products are produced in 25 different plants around the world, managed through our rigorous quality system and subject to internationally recognized certifications such as the Food Safety System Certification FSSC 22000.
Discover more at www.fssc.com.
Kinder products are produced in 25 different plants around the world, managed through our rigorous quality system and subject to internationally recognized certifications such as the Food Safety System Certification FSSC 22000.
Discover more at www.fssc.com.